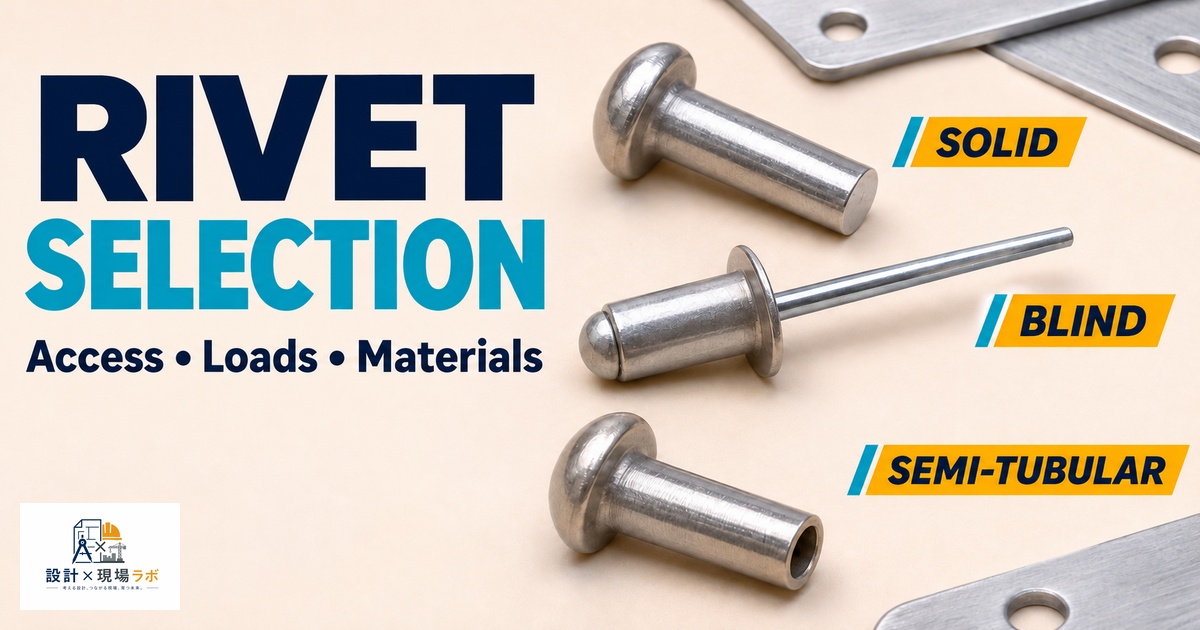
Twenty years of working as a contract mechanical designer inside Japanese manufacturing plants has taken me through automotive brackets, HVAC sheet metal assemblies, and a long stretch on consumer appliance chassis, and rivets have followed me through all of it. They get treated as an afterthought compared to welding or bolted joints, something you specify at the very end of a drawing package almost as a formality. That is a mistake. Choosing the wrong rivet type, or sizing one incorrectly for the joint’s shear and tensile loads, has caused more field failures on projects I have touched than almost any other single fastener decision. This article covers how I choose between solid, blind, and semi-tubular rivets, and the practical considerations that do not always make it into a fastener catalog.
- Solid Rivets: Still the Standard for High-Strength Structural Joints
- Blind Rivets: The Default When Only One Side Is Accessible
- Semi-Tubular Rivets: Built for Automated, High-Volume Assembly
- Sizing for Shear and Tensile Load
- Edge Distance and Hole Spacing
- Material Compatibility and Galvanic Corrosion
- Head Style and Aesthetic or Clearance Constraints
Solid Rivets: Still the Standard for High-Strength Structural Joints
Solid rivets are the oldest style and, in my experience, still the right answer whenever a joint needs to carry serious shear or vibration loads and both sides of the joint are accessible during assembly. A solid rivet is a single shaft with a preformed head on one end; the other end is upset (deformed) with a hammer, squeeze tool, or hydraulic press to form the second head, clamping the stack tightly. On a chassis bracket program for an industrial cart, we used solid rivets specifically because the joint saw cyclic vibration loading during transport testing, and solid rivets fill the hole more completely and consistently than a blind rivet’s mandrel-driven body, giving a tighter, more fatigue-resistant joint.
The tradeoff is obvious but still underestimated: you need access to both sides. On a project I worked on early in my career, a junior designer specified solid rivets for a sheet metal enclosure seam where one side was a closed box section — nobody could get a bucking bar or die in to form the second head. The design had to be reworked late, after the tooling for the enclosure was already committed, because the accessibility issue was not checked until the assembly line trial. I still start every rivet joint review by asking a simple question: can a technician physically reach both sides of this joint with a tool? If the answer is no, solid rivets are off the table before any strength calculation matters.
Blind Rivets: The Default When Only One Side Is Accessible
Blind rivets (often called pop rivets, though that is technically a brand name) are what I reach for whenever the joint is a closed section, a box, or anything where the back side is inaccessible during final assembly. A blind rivet has a mandrel running through a hollow rivet body; pulling the mandrel with a rivet tool deforms the far end into a blind head while the near side seats against the flush head, and the mandrel then snaps off. I once ran into a case where a design review flagged a control box lid assembly for excessive vibration-induced loosening, and the root cause turned out to be a standard open-end blind rivet used in a location that saw repeated thermal cycling — the mandrel had backed partially out over several hundred cycles, reducing clamp force. Switching to a closed-end (sealed) blind rivet, which traps the mandrel stub inside a sealed cavity rather than leaving a hollow shaft, solved both the loosening and a secondary water-ingress complaint we had not even connected to the same root cause at first.
Blind rivets come in more sub-variants than most engineers realize, and picking the right one matters. Standard open-end rivets are cheapest and fine for static, low-load applications. Closed-end (sealed) rivets cost more but resist moisture and vibration loosening far better. Structural blind rivets, which use a thicker-walled body and a different mandrel-lock mechanism, can approach solid rivet shear strength and are what I specify whenever a blind-access joint also needs to carry real structural load, such as a mounting bracket on outdoor equipment.
| Rivet type | Access needed | Typical shear strength range | Common use case |
|---|---|---|---|
| Solid rivet | Both sides | Highest, most consistent | High-vibration structural joints |
| Standard blind rivet | One side | Moderate | Light sheet metal, low load |
| Sealed blind rivet | One side | Moderate | Enclosures needing moisture resistance |
| Structural blind rivet | One side | Near solid-rivet levels | Blind-access structural brackets |
| Semi-tubular rivet | Both sides (typically) | Moderate, ductile | High-volume automated assembly |
Semi-Tubular Rivets: Built for Automated, High-Volume Assembly
Semi-tubular rivets have a partially hollow shank on the driven end, which reduces the force needed to upset the head compared to a fully solid rivet of the same diameter. This matters enormously in high-volume automated assembly, and it is where I have specified them most often — on an automotive interior trim line running tens of thousands of units, the reduced setting force meant the riveting head on the automated cell could cycle faster and with less wear on the tooling than a solid-rivet setup would have required for the same diameter.
The strength tradeoff is real, though smaller than people expect if the hollow depth is chosen correctly. A semi-tubular rivet with a shallow hole depth (say, 25% of the shank length) loses relatively little shear strength compared to a solid rivet, while a deep-hole version loses considerably more. On a bracket redesign where a supplier had substituted a deep-hole semi-tubular rivet for a solid rivet to cut tooling force without telling us, the joint passed initial static testing but failed a fatigue test about 60% earlier than the original design. We traced it to the reduced cross-section at the shank concentrating stress differently than the original solid rivet had. The lesson I took from that, and repeat to anyone who will listen, is that a rivet substitution is never a drop-in change without re-verifying the load case, even when the outer diameter and length on the spec sheet match.
Sizing for Shear and Tensile Load
The core calculation for any rivet joint starts with identifying whether the load path is primarily shear (loads acting parallel to the rivet’s cross-section, as in a lap joint) or tension (loads trying to pull the rivet axially, as in a butt joint with a strap). Most sheet metal riveted joints I design are single-shear or double-shear lap joints, and the allowable load is essentially the rivet’s shear strength (a material property, roughly 0.6 times the tensile strength for many aluminum and steel rivet alloys) multiplied by the shear area, divided by a safety factor appropriate to the application — I typically use 3 to 4 for structural brackets subject to dynamic loading, lower for purely static, redundant joints.
Diameter selection also has to respect the sheet thickness being joined, not just the calculated load. A rule of thumb I use for sheet metal riveting is that rivet diameter should be roughly 2.5 to 3 times the thickness of the thinner sheet in the joint, mostly to avoid the sheet material tearing out around the rivet hole before the rivet itself fails — a failure mode that a pure shear-strength calculation on the rivet alone will not catch. On a thin-gauge aluminum panel assembly, we originally sized rivets purely off the shear load calculation and specified a smaller diameter than the sheet-thickness rule would have suggested; prototype testing showed the panel tearing out around the rivet head under load well before the rivet itself reached its rated shear capacity, and we had to increase diameter and add a backing washer to spread the bearing load.
Edge Distance and Hole Spacing
Edge distance — how far the rivet hole sits from the edge of the material — is one of those details that seems minor until it causes a field failure. Too little edge distance and the sheet material can tear out from the hole to the free edge under load, regardless of how strong the rivet itself is. My working minimum is two times the rivet diameter from hole center to the nearest free edge, and I push for 2.5 times when the material is a lower-ductility aluminum alloy that does not deform gracefully before tearing.
Spacing between adjacent rivets in a multi-rivet joint matters for a different reason: too close together and you get stress interaction between the holes that reduces the net section strength of the sheet more than a simple hole-area subtraction would predict. I generally keep rivet spacing at a minimum of three times the diameter, center to center, and closer to four times when the joint sees fatigue loading rather than purely static load. On a bracket with rivets spaced at roughly 2.2 diameters apart because of a tight packaging constraint, we saw the sheet crack along the rivet row during endurance testing well before the individual rivets showed any distress — the fix required widening the bracket slightly to get proper spacing, which was a costly late-stage change that a spacing check early in the layout would have avoided entirely.
Material Compatibility and Galvanic Corrosion
Rivet material selection is not just about strength; it is about what it is being riveted to. I have seen galvanic corrosion cause more warranty issues in outdoor and automotive-adjacent products than almost any other rivet-related problem. Aluminum rivets in steel sheet, or steel rivets in aluminum sheet, set up a galvanic couple in the presence of moisture, and the less noble metal corrodes preferentially — often the rivet itself, which then loosens the joint from the inside out. On an outdoor equipment bracket program, we had originally specified plain steel blind rivets into an aluminum frame purely because they were cheaper and readily available from the assembly plant’s existing stock. Field returns after about eighteen months in humid coastal regions showed rivet corrosion and joint loosening that a simple material compatibility check at the design stage would have caught. Switching to stainless steel rivets, or matching aluminum rivets to the aluminum frame with a compatible coating, resolved it, but only after a costly recall-adjacent retrofit campaign.
Head Style and Aesthetic or Clearance Constraints
The last consideration I want to cover, because it gets overlooked in favor of pure strength calculations, is head style. Round head, countersunk (flush), and low-profile head rivets are not interchangeable even when the shank strength is identical, because the head geometry affects both clearance and load distribution. Countersunk rivets require a chamfered hole and generally have somewhat lower pull-through resistance than a round or truss head of the same diameter, because there is less material under the head to resist the sheet pulling over it. On an appliance panel where a flush exterior surface was required for aesthetic reasons, we specified countersunk rivets and had to increase the diameter slightly compared to what a round-head rivet would have needed, specifically to compensate for the reduced pull-through resistance the countersunk geometry introduced. It is a small detail, but it is exactly the kind of tradeoff that separates a rivet joint that survives its service life from one that does not, and it only takes a few extra minutes at the drawing stage to get right.
コメント