
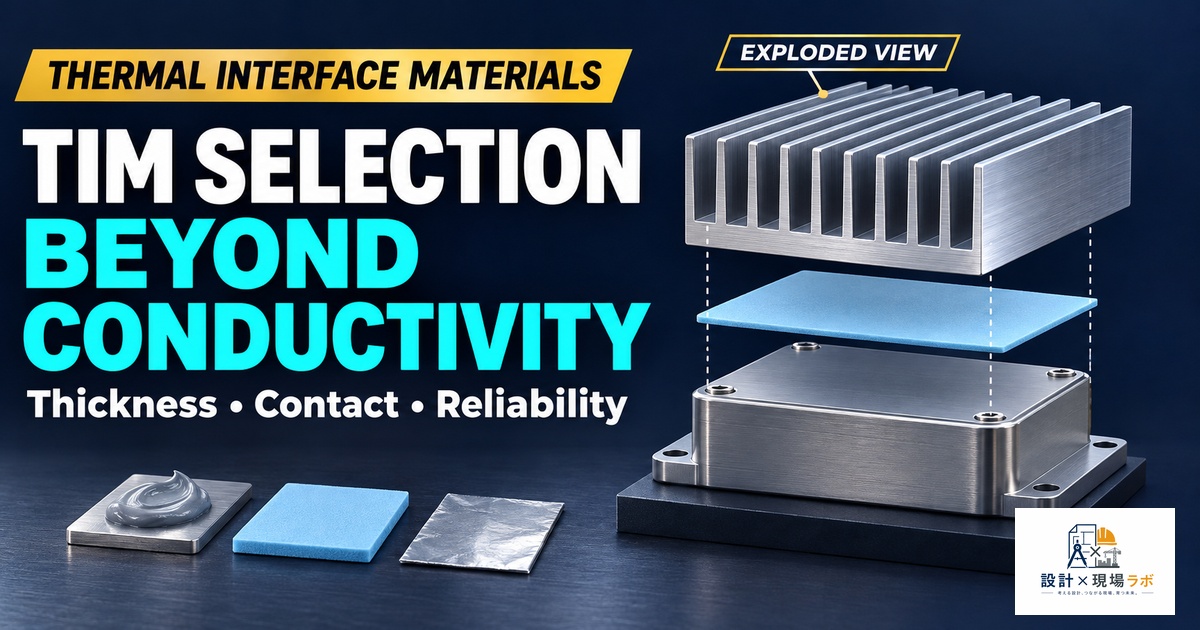
If there’s one component category I’ve watched engineers underestimate more consistently than any other, it’s the thermal interface material. A TIM is usually the thinnest, cheapest item in the whole thermal stack, and yet it can single-handedly determine whether a design meets its junction temperature target or fails thermal qualification. I’ve spent more hours than I’d like to admit staring at thermal camera images trying to figure out why a perfectly good heat sink wasn’t pulling its weight, only to trace the problem back to a TIM that was applied wrong, specified wrong, or simply the wrong material for the job. This article is a rundown of what I’ve learned selecting and applying TIMs across two decades of mechanical design work inside manufacturing environments.
Why TIMs Matter: The Air Gap Problem
No two mating surfaces are perfectly flat or perfectly smooth, no matter how tightly you control your machining tolerances. At a microscopic level, every interface between a component case and a heat sink is a landscape of peaks and valleys, and the actual contact area between two “flat” metal surfaces pressed together is often only a few percent of the nominal area. The rest is air, and air is a terrible thermal conductor, somewhere around 0.026 W/m·K. A TIM’s entire job is to fill those microscopic gaps with something that conducts far better than air, even if that something is itself a mediocre conductor compared to metal.
This is why bulk thermal conductivity numbers on a TIM datasheet can be misleading if taken in isolation. I once worked with a design team that selected a TIM based purely on the highest conductivity value in a vendor comparison chart, without accounting for how thick a bond line that particular material required to be applied reliably in production. The high-conductivity option needed a thicker layer to avoid pump-out over time, and once you factor in bond line thickness, its effective thermal resistance ended up worse than a lower-conductivity pad that could be applied much thinner. Thermal resistance, not conductivity alone, is what actually matters at the interface.
Types of TIMs and Their Trade-offs
Thermal grease remains the go-to for the lowest achievable thermal resistance because it can be applied in extremely thin bond lines, often under 50 microns, and it conforms well to surface irregularities. The trade-off is application consistency — grease is messy, operator-dependent in manual assembly, and prone to pump-out or dry-out over years of thermal cycling, especially in applications with significant vibration.
Thermal pads trade some performance for enormous gains in manufacturability. They come in fixed thicknesses, which is genuinely useful when you need the TIM to also take up a mechanical tolerance gap between a component and a heat sink, not just conduct heat. I’ve used pads specifically for that dual purpose on stacked PCB assemblies where the gap to the enclosure varied by a millimeter or more across the tolerance stack, and a pad simply compressed to fill whatever gap existed at each unit.
Phase change materials sit in an interesting middle ground: solid and easy to handle at room temperature like a pad, but they melt at operating temperature and flow to fill surface irregularities almost as well as grease. I’ve had good results with PCMs on power modules that ran hot enough to trigger the phase transition reliably during first power-on, but I’ve also seen problems on designs where the component never got hot enough in normal operation to fully activate the material, leaving performance stuck at the pre-melt state.
Graphite sheets and metal-based TIMs like indium foil occupy the high-performance end, with indium in particular offering excellent conductivity and the ability to conform under pressure without the long-term reliability concerns of grease. The cost and handling complexity usually restrict these to applications where the thermal budget genuinely has no room left, like RF power amplifiers or high-density processor modules.
Application Process and Common Mistakes
I cannot count the number of times a thermal problem on a production line traced back to application technique rather than material selection. Too much grease and you end up with a thick, non-uniform bond line that defeats the purpose of choosing a low-resistance material in the first place. Too little and you leave dry spots where the microscopic air gaps never get filled at all. The classic dot or X pattern taught in most assembly training works reasonably well for smaller die sizes, but for larger interface areas I’ve had better and more repeatable results specifying a controlled dispense volume with a thin, even spread pattern applied by a semi-automated dispensing head, particularly once we scaled past low-volume prototype builds.
Pad application seems foolproof by comparison, but I’ve seen assembly errors there too — pads installed with the adhesive liner still attached, pads compressed beyond their rated deflection because the fastener torque wasn’t controlled, and pads that migrated slightly during assembly because they weren’t tacky enough to stay registered before the mating surface came down. On one project, we added a simple locating feature stamped into the heat sink specifically to keep the pad from shifting during the automated press step, which eliminated a intermittent quality escape that had been showing up as random field failures.
Pump-Out and Long-Term Reliability
Grease pump-out is a slow, insidious failure mode that rarely shows up in short qualification testing but can devastate field reliability over years. Repeated thermal cycling causes differential expansion between the component and heat sink, effectively pumping grease out of the interface a tiny amount with every cycle until voids form and thermal resistance climbs. I worked on a product where field returns after three to four years in service showed a consistent pattern of elevated case temperatures traced to grease pump-out at a fastener interface that saw unusually large thermal cycling amplitude due to its mounting location near an enclosure vent.
The fix in that case was switching to a phase change material with better pump-out resistance for that specific interface, while keeping grease elsewhere in the design where cycling amplitude was lower and the risk was acceptable. This is a good example of why I resist standardizing on a single TIM for an entire assembly — different interfaces in the same product can have meaningfully different thermal cycling profiles, and the TIM selection should reflect that rather than defaulting to whatever the purchasing department already has on the shelf.
Selecting TIM for Specific Applications
| Application characteristic | Reasonable TIM choice | Why |
|---|---|---|
| Large tolerance stack-up gap | Thermal pad | Fills variable gap, easy to handle |
| Highest possible performance, low volume | Indium foil or high-end grease | Cost justified by thermal budget |
| High vibration, long service life | Phase change material | Better pump-out resistance than grease |
| High-volume automated assembly | Pre-cut pad or dispensed grease | Process repeatability |
| Rework expected during service life | Reusable pad, not grease | Cleaner disassembly |
Beyond this kind of general mapping, I always try to get an actual sample of the interface geometry — a representative fixture or an early prototype — before locking in a TIM decision, because surface finish and flatness on the real parts frequently differ from what the CAD model assumes, and that difference matters more for TIM performance than most other tolerances in the stack.
Testing and Validation
The only reliable way I’ve found to validate a TIM decision is direct thermal measurement on representative hardware, ideally with a thermocouple or thermal camera reading at the actual junction or case temperature, not an inferred number from an ambient reading. Datasheet thermal resistance values are measured under controlled, ideal conditions with specified pressure and bond line thickness that your assembly may not actually achieve. I’ve seen designs pass on paper using datasheet numbers and then run 8 to 10°C hotter than predicted in the field because actual applied pressure from the fastener pattern was lower than the test condition assumed.
Whenever possible, I push for accelerated thermal cycling on the actual TIM and interface combination before it locks into production, specifically watching for the pump-out and dry-out behavior that short-duration testing simply won’t reveal. It’s a small extra step in a schedule that always feels tight, but the cost of a thermal-related field failure years into a product’s life is far higher than the cost of that testing up front, and I’ve had to learn that lesson the hard way more than once over the years.
Reference
Thermal design questions tend to come back to the same handful of heat transfer fundamentals.
Fundamentals of Heat and Mass Transfer (Incropera)
As an Amazon Associate I earn from qualifying purchases.
コメント